
Steel Pipe Procurement: How Do You Estimate Quantity Correctly?
An under-quoted tonnage stops a shipment at the port; an over-quoted one ties up working capital. Steel pipe procurement quantity is a calculation, not a guess.
You estimate steel pipe procurement quantity by converting the line list into theoretical weight — length multiplied by unit weight derived from outside diameter and wall thickness — then adding allowances for cutting, testing and wall tolerance, and checking the total against transport payload limits.
Transition: a tonnage is only the last line of a longer calculation. Behind that number sit a line list, a set of mill lengths, a tolerance band, a cutting plan and a vessel or container that will refuse to carry more than its payload. The six sections below follow that chain in order — what a quantity decision really controls, how to convert a line list into an order, how theoretical weight is calculated, what manufacturing practice does to the ordered figure, where importers most often lose money, and what belongs in the enquiry itself.
What Does Quantity Estimation in Steel Pipe Procurement Actually Decide?
Before a single tonne is quoted, quantity estimation fixes the order unit, the shipping method and much of the payment structure.
Pipe is bought by weight, manufactured by length and transported by payload. A quantity that ignores mill lengths, cutting losses or payload limits changes the landed cost of the line, not just the invoice value.
Three units sit behind one quantity
Steel pipe is priced by weight, produced by length and shipped by payload, so a purchase order carries three numbers that must agree with one another: a tonnage for the commercial side, a piece count or total length for production planning, and a volume that tells the forwarder whether the cargo fits the equipment already booked. When only the tonnage is negotiated, the other two are resolved later — by the supplier, at the supplier’s convenience. That is where avoidable differences appear. A mill that supplies six-metre lengths instead of twelve turns one straight run into twice as many joints, twice as many field welds and a different bill of materials for the fabricator, even though the tonnage on the contract is identical.
Why the estimate constrains the negotiation
Quantity also determines which offers you can consider at all. Small tonnages attract mill surcharges or are routed to stockists with a trading margin built in; larger tonnages open direct mill allocation, better payment terms and sometimes a rolling programme instead of a single heat. The same specification quoted at thirty tonnes and at three hundred tonnes is not the same commercial product, and a buyer who has not fixed the quantity before requesting prices is comparing offers that were never comparable in the first place.
What a good estimate is not
An estimate is not a promise about final weight. It is a planning figure with a stated basis: this outside diameter, this wall thickness, this length per joint, these allowances, that payload. If the basis is written down, any difference between estimate and delivery can be traced back to a decision — a tolerance clause, a cutting plan, a change of length requested after the order was placed. If the basis is not written down, the same difference becomes an argument about who was wrong. Writing the basis into the enquiry costs ten minutes and converts the whole quantity discussion from opinion into verification.
How Do You Convert a Pipe Line List into Orderable Quantities?
A line list describes service, diameter, wall and route length. Quantity estimation turns that description into something a mill can actually roll and deliver.
Work line by line: convert each route length into the number of standard lengths required, round up to whole lengths, and total by size and wall. Only after the piece counts are fixed should you convert those totals into weight.
Step one: freeze the specification on every line
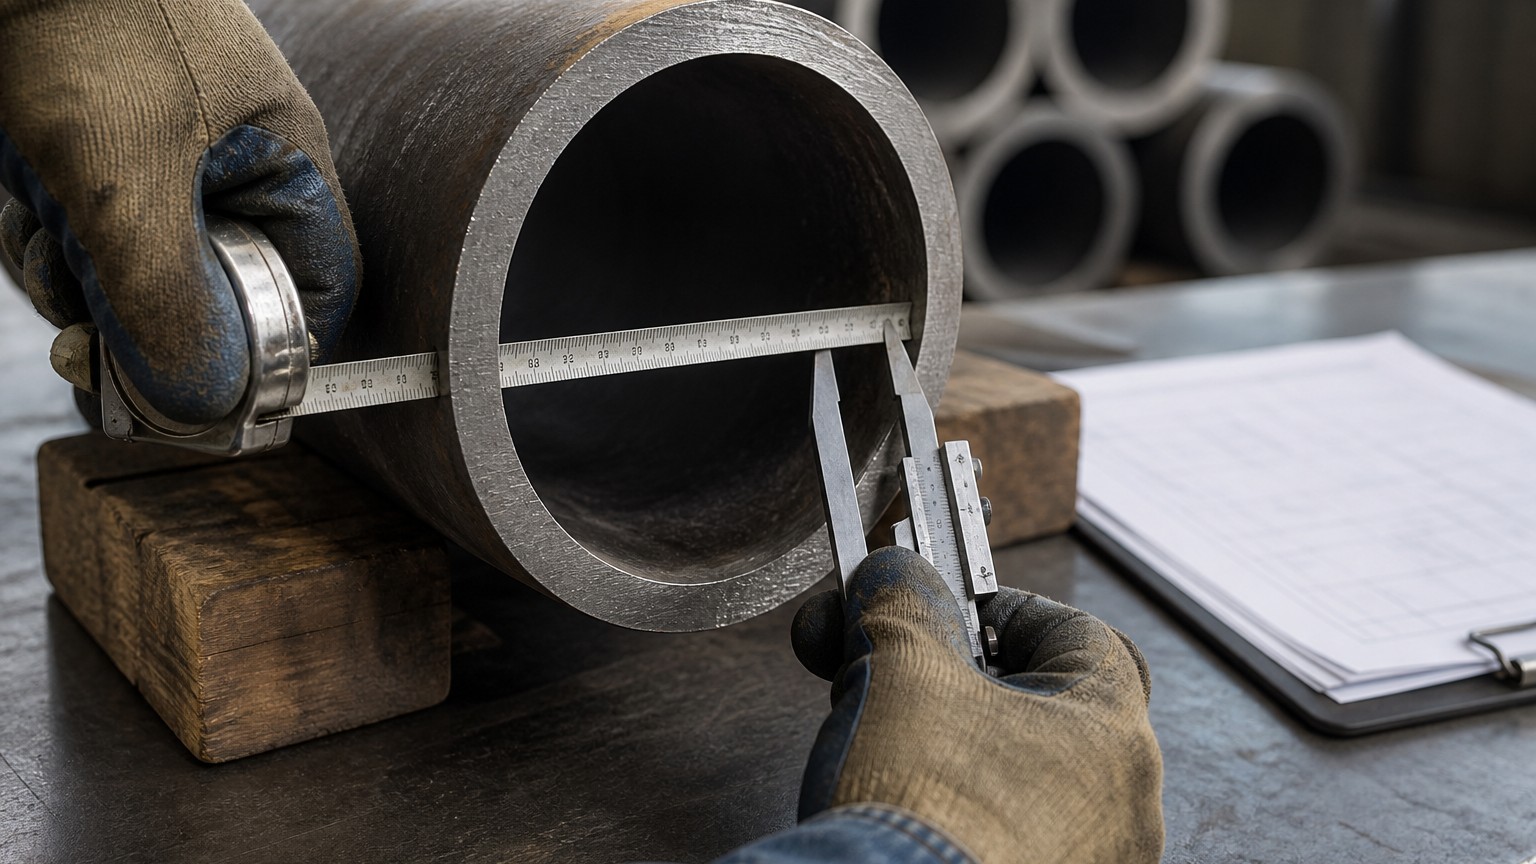
Every line must be pinned to a diameter and a wall designation before any quantity means anything, and the two must be read together. A diameter without a wall thickness is not a pipe, and the fastest way to check whether a specification is complete is to look for the schedule. Buyers who inherit a line list regularly find entries such as “nominal 6 inch” with no schedule attached; that single omission can move the weight of the same route by a large multiple, because outside diameter is fixed by the size designation while wall thickness rises with the schedule. NPS 6 at Sch 40 has an outside diameter of 6.625 inches (168.3 mm) and a wall of 0.280 inches (7.11 mm); NPS 6 at Sch 80 keeps the same outside diameter but thickens the wall to 0.432 inches (10.97 mm), which is roughly half again the weight per metre for identical length. Freeze both numbers on the line list before any multiplication begins, and use the reference on how pipe dimensions and wall thickness are written if a specification mixes inch and metric conventions.
Step two: convert route length into standard lengths
Random lengths and fixed lengths behave differently, and neither is a continuous reel. A route of 137 metres is not 137 metres of order; it is a whole number of joints plus the remnant you discard when the final piece comes up short. Round up per line, never per project, because sizes cannot be mixed to make up a shortfall — a surplus of NPS 4 cannot reduce the number of NPS 6 joints required. Where the route includes fittings, valves and flanges, remember that each fitting consumes a length of its own, and a cutting plan built from a drawing without those take-outs will be short every time. Recording the piece count per line alongside the length is what allows the supplier to confirm whether the order will be produced from stock lengths or cut to a stated fixed length, and that decision changes both the price and the delivery date.
Step three: attach allowances to the line that creates them
Allowances are not uniform across a project. A straight run of pipe that will be butt-welded in the field needs almost nothing beyond the cutting loss at each joint; a line that will be cut, threaded, bevelled, hydro-tested and re-cut after a failed test consumes a different order of material. Separating allowances line by line rather than padding a single project total preserves the audit trail. When the delivered weight later differs from the estimate, the line responsible is immediately visible, which is impossible if every line has been inflated by a project-wide percentage. It also prevents the common error of adding a cutting allowance to a line that is being supplied cut to length by the mill in the first place.
Step four: keep a net column and an order column
Maintain two columns for every line: the net calculated quantity and the order quantity after allowances. Report both in the internal procurement file and quote only the order figure commercially. This habit costs nothing and answers the two questions that always arrive together — how much material does the design need, and how much are we actually buying. It also makes later change orders defensible: when a scope change adds forty metres to a route, the additional quantity is calculated from the same stated basis as the original, rather than renegotiated from scratch on a new assumption.
How Do You Turn Pipe Dimensions into Weight and Tonnage?
Theoretical weight is the bridge between a line list and a purchase order, and it is only ever as accurate as the dimensions fed into it.
For carbon steel pipe, theoretical unit weight in kilograms per metre is calculated as 0.02466 multiplied by the wall thickness in millimetres and by the outside diameter minus the wall thickness in millimetres. Multiply by the total length to obtain order weight.
What the formula assumes, and when to stop using it
The constant 0.02466 is not a fudge factor; it is the density of steel expressed in units that match the dimension inputs. The cross-sectional area of a pipe wall in square millimetres is π multiplied by the wall and by the outside diameter minus the wall; converting millimetres to metres and cubic millimetres to kilograms at a density of 7.85 grams per cubic centimetre collapses the whole relationship into a single multiplier. That is why the formula works in millimetres and kilograms and why it stops being accurate the moment the material is no longer carbon steel. Stainless steel is denser than carbon steel, so a stainless pipe of identical diameter and wall weighs more per metre, and the density of the specific grade has to be substituted before the tonnage is used for a commercial commitment. The second assumption is more subtle: the formula describes a pipe at nominal dimensions, so it returns theoretical weight rather than weighed weight. The two agree closely on a compliant order, but they are different quantities, and a purchase order written on theoretical weight should say so, because a mill weighing actual bundles will always be able to show a difference and the tolerance clause in the product standard is what decides whether that difference is acceptable. The third point of care is unit discipline. Mixing inch wall thicknesses with millimetre diameters in the same calculation is the single most common arithmetic failure in quantity estimation, and it is invisible in the output because the number looks plausible.
A worked weight table for common sizes
The table below applies the carbon steel formula to five sizes in Sch 40, using nominal dimensions. Values are theoretical, calculated rather than weighed, and are shown to one decimal place.
| Nominal size | Outside diameter mm | Sch 40 wall mm | Theoretical unit weight kg/m | Theoretical weight of one 6 m length kg |
|---|---|---|---|---|
| NPS 3 | 88.90 | 5.49 | 11.3 | 67.8 |
| NPS 4 | 114.30 | 6.02 | 16.1 | 96.4 |
| NPS 6 | 168.28 | 7.11 | 28.3 | 169.6 |
| NPS 8 | 219.08 | 8.18 | 42.5 | 255.2 |
| NPS 12 | 323.85 | 10.31 | 79.7 | 478.3 |
The practical use of a table like this is comparison, not precision. Multiply unit weight by total length in metres, per line, and you have the order weight for that line; total the lines and you have the project figure. The same nominal size also illustrates how the wall governs the money: NPS 3 at Sch 40 is about 11.3 kilograms per metre, and the same nominal size at a heavier schedule rises in step with the wall while the outside diameter stays exactly where it was. Where the order covers several schedules of one size, keep the schedules on separate rows rather than averaging them, because an average hides the line that will need the heaviest lifting equipment and the largest transport allowance. The reference tables behind these figures follow the dimensional conventions of the international pipe standards, and a fuller set of conversions is available on our seamless steel pipe pages, where sizes, walls and standards are stated together as they would appear on a mill offer. The dimensional background itself is summarised in the open reference material on Nominal Pipe Size, which tabulates outside diameter and wall thickness across the schedule range for the small and medium sizes that dominate general trade.
What Do Tolerances and Mill Practices Do to the Ordered Quantity?
Nominal figures are design values, and manufacturing moves around them. The ordered quantity has to absorb that movement consciously rather than accidentally.
Wall thickness is a nominal value that may vary over or under the nominal figure, and length, straightness and end finish are governed by the specification you order to. Place the allowance where the variation occurs instead of padding the whole order.
Where the variation actually appears
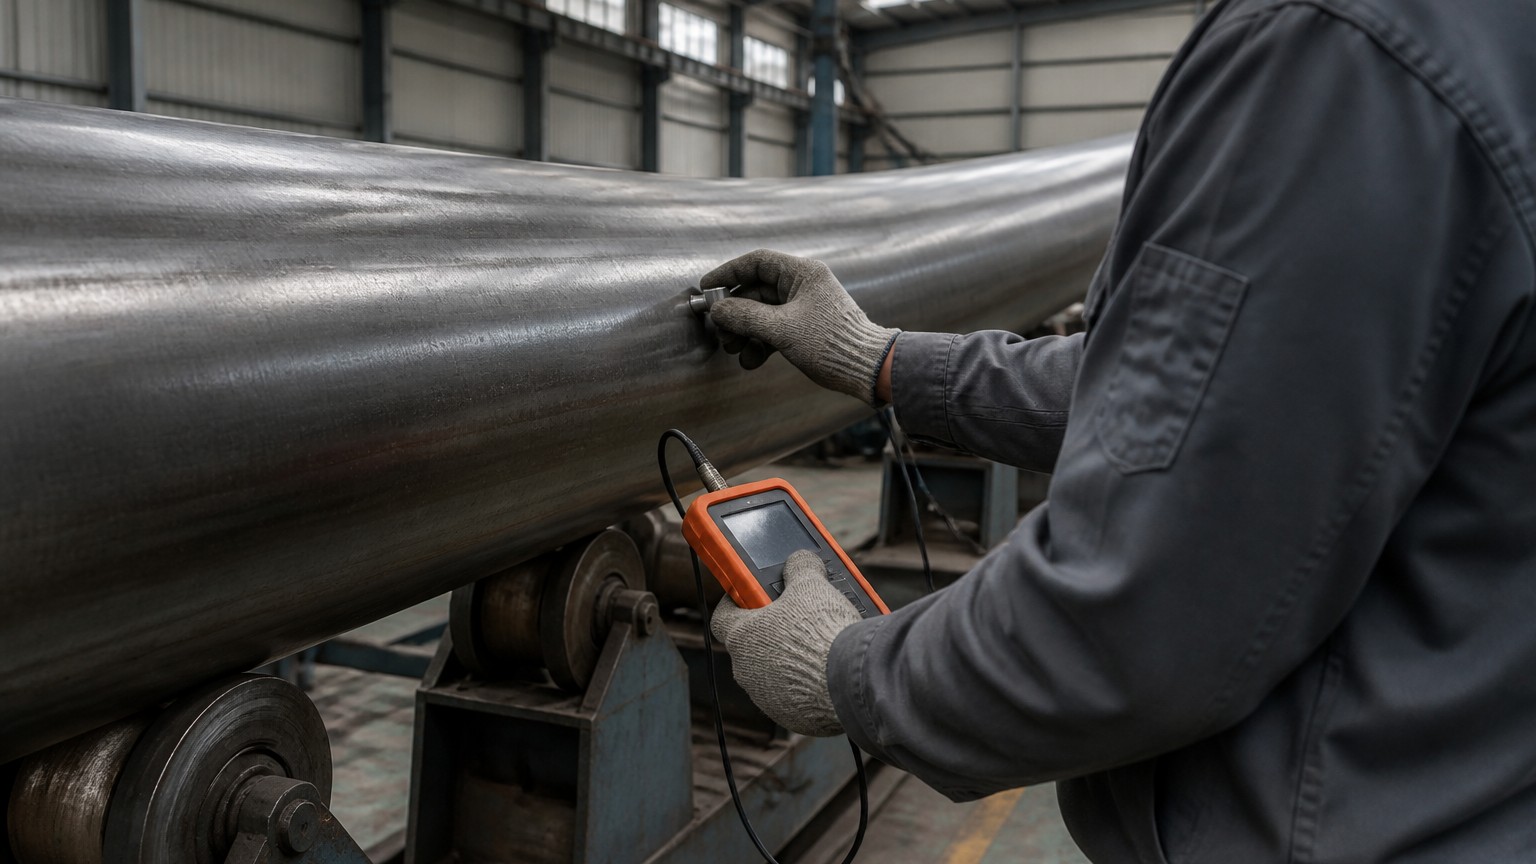
Three properties move, and each moves for its own reason. Wall thickness varies within a permitted band, and the standards are explicit that the nominal wall is a name rather than a measurement: the note in ASTM A53/A53M states that the term nominal wall thickness exists in name only and is used to distinguish it from the actual wall, which may vary over or under the nominal value. Outside diameter moves within its own band, and it is the dimension that decides whether fittings assemble. Length moves as well, because mill output comes in random lengths within a stated range unless a fixed length is ordered, and the range is wide enough to change a cutting plan. Confirming which wall belongs to a given schedule before the tolerance clause is agreed takes a minute with the schedule chart that maps nominal size to wall thickness across the size range. A quantity built on nominal dimensions without a tolerance clause is therefore accurate only in theory. Two responses are available. The first is to buy on theoretical weight and accept that the delivered weight will differ slightly within specification. The second is to buy on actual weighed weight, which shifts the tolerance risk to the supplier’s side of the table and usually costs something in price. Either is defensible; leaving the question unstated is not, because the two approaches produce different invoice values for the same physical order.
Testing and end preparation consume quantity too
Testing is a material event, not just a paperwork step. Destructive tests remove material from the order: a length cut for a tensile or bend specimen is no longer a deliverable joint, and the standard under which the pipe is bought determines how many tests are taken per lot and therefore how much is consumed. Non-destructive methods such as ultrasonic or eddy-current inspection leave the material intact but require the ends to be clean and accessible, and a failed test on a joint triggers re-testing or rejection of that piece. End preparation follows the same logic. A bevelled end, a threaded end or a grooved end is a fabrication operation that changes how the joint is counted and packed, and where ends are protected with caps or thread protectors for shipment, the protectors themselves appear in the packing list and therefore in the freight calculation. None of these items is large individually; together on a multi-line import order they are the difference between an estimate that holds and one that needs a change order in the first week of shipping.
Documentation is part of what you are buying
The quantity you order also determines the documentation set you can reasonably expect. A single heat rolled for one line produces a short, clean certificate trail; a large programme assembled from several heats produces a certificate set that must be reconciled heat by heat against bundles and lengths. Where the material is bought against an international oil and gas standard, the applicable specification range is published by the American Petroleum Institute standards programme, and the scope of testing stated there is what makes a heavier documentation package necessary on some lines and not on others. Buyers who plan the certificate requirement at the quotation stage avoid the position of discovering, at loading, that the supplier’s standard certificate cannot be mapped to their own incoming inspection procedure.
Where Do Importers Lose Money in Quantity Estimation?
Most quantity losses are not arithmetic mistakes. They are unit, payload, packing and classification decisions taken after the tonnage was already fixed.
The recurring leaks are allowances counted twice, payload limits noticed too late, packing weight handled inconsistently, and classification errors that change the duty payable on arrival.
Leak one: the same allowance added twice
Allowances accumulate silently when different people apply them at different stages. The design engineer adds a cutting allowance, the procurement officer adds a safety margin, and the supplier rounds the order up to whole bundles — three reasonable decisions that together can overshoot a modest proportion of the order value. On a heavy line, the surplus is not just money: it is extra freight, extra lifting, extra storage and, in some jurisdictions, extra duty. The defence is procedural rather than mathematical. Record who added what, keep the net and order columns separate, and state in the enquiry which allowances are already included. A supplier who knows that a stated figure already contains a cutting allowance will not add a second one, and a quotation that is silent on the point should be questioned before it is signed.
Leak two: the payload wall arrives before the container is full
Pipe is a weight-dense product, so a container or truck reaches its maximum payload long before it runs out of volume. An import plan built on cubic capacity alone will produce a quantity that cannot be shipped in the equipment booked, and the remedy is a second shipment at full freight cost. The check is straightforward and belongs in the estimate itself: convert the tonnage into a number of container or truckloads using the payload your forwarder confirms for the route and the equipment, and if the last unit is half empty, adjust the packing plan or the release schedule rather than the total. Releasing a large order in two shipments also changes the cash-flow profile and the storage position at destination, both of which belong in the landed cost comparison that justified the order in the first place.
Leak three: packing and bundling handled inconsistently
Packing has weight, and weight is what you pay for. Bundles banded with steel straps, wooden cradles, end caps and thread protectors all add mass, and the way the supplier declares that mass varies. Two suppliers quoting the same net tonnage can therefore deliver different invoice tonnages for the same pipe. Ask for the packing method and the declared gross weight in the offer, state it in the order, and keep it identical when comparing suppliers. Where the material will be stored outdoors at destination, the packing specification is a cost decision as well as a weight decision, and it should be taken deliberately rather than accepted by default.
Leak four: classification decided after the price was agreed
Duty is calculated on the value of the goods as classified, and classification is not a description exercise. The Harmonized System is administered by the World Customs Organization and revised every five years, and the six-digit subheading is common across participating countries while individual countries add further digits for their own tariff treatment — a structure set out in the guidance published by the US International Trade Administration. Because the first six digits are shared internationally, a classification agreed with one supplier is reusable with another, but only if the product description actually supports it. A pipe described as a line pipe, a structural tube or a boiler tube can sit under different subheadings, and an incorrect classification discovered at destination produces duty adjustments, storage costs and delays that dwarf the quantity precision the order was built on. Agreeing the classification code with the forwarder before the order is placed takes an afternoon and removes the largest single source of unexpected landed cost in a steel pipe programme.
What Should a Steel Pipe Procurement Enquiry Include?
A complete enquiry is short, and it prevents the round of re-quoting that quietly consumes the first week of every project.
Send the nominal size, wall or schedule, grade or governing standard, total length per line, length per joint, end finish, quantity basis and delivery terms, then state which allowances you have already included in the figure.
The line items that remove most questions
Six entries answer almost every query a mill will raise. State the size and schedule together, because one without the other is not a specification. State the standard and grade the pipe is to be produced and tested to, since the same dimensions can be supplied under different testing regimes. State the total length and the length per joint, and say whether the total is a net route length or an order length already rounded to whole joints. State the end finish and whether the ends are to be plain, bevelled, threaded or protected. State the quantity basis: theoretical weight, actual weight, or pieces. Finally state the delivery terms and the destination port, because the packing method and the transport unit both depend on the route. A line that reads Carbon Steel Pipe 20# 3 inch Sch 40, for example, fixes the size, the schedule and the grade designation in a single phrase and leaves nothing to interpretation at the quotation stage.
Say what the number includes
The allowance statement is the most valuable line in the enquiry and the one most often omitted. “Two hundred and forty metres, net of cutting loss, plus a three per cent cutting allowance” is unambiguous. “Two hundred and forty metres, roughly” is not, and it will be interpreted in the supplier’s favour or against you depending on which way the market is moving. When the basis is stated, competing offers become directly comparable, because each supplier is pricing the same quantity under the same assumptions, and the only differences left on the table are the ones you actually want to negotiate: price, tolerance, packing, testing and delivery. It also gives you a defensible position if the delivered weight differs from the estimate, because the difference can be attributed to a named clause rather than to the buyer’s arithmetic.
What a good answer returns
A competent quotation comes back with more than a price. It states the unit weight basis used, the length per joint that will be supplied, the tolerance clause the pipe will be produced to, the packing method and the certificate package. When those five items are present, the quantity estimate can be reconciled against the offer line by line before the order is placed, and the reconciliation is the cheapest risk control available on a steel pipe import programme. If you want the weight basis, the length per joint, the tolerance statement and the packing plan confirmed against a specific line list before you commit, send your line list and quantities to our export team and we will return a worked figure with the assumptions shown.
Conclusion: How Should You Estimate Steel Pipe Procurement Quantity?
Freeze size and wall first, convert length into whole mill lengths, calculate weight from nominal dimensions, place allowances where the variation occurs, and check the tonnage against payload before signing.